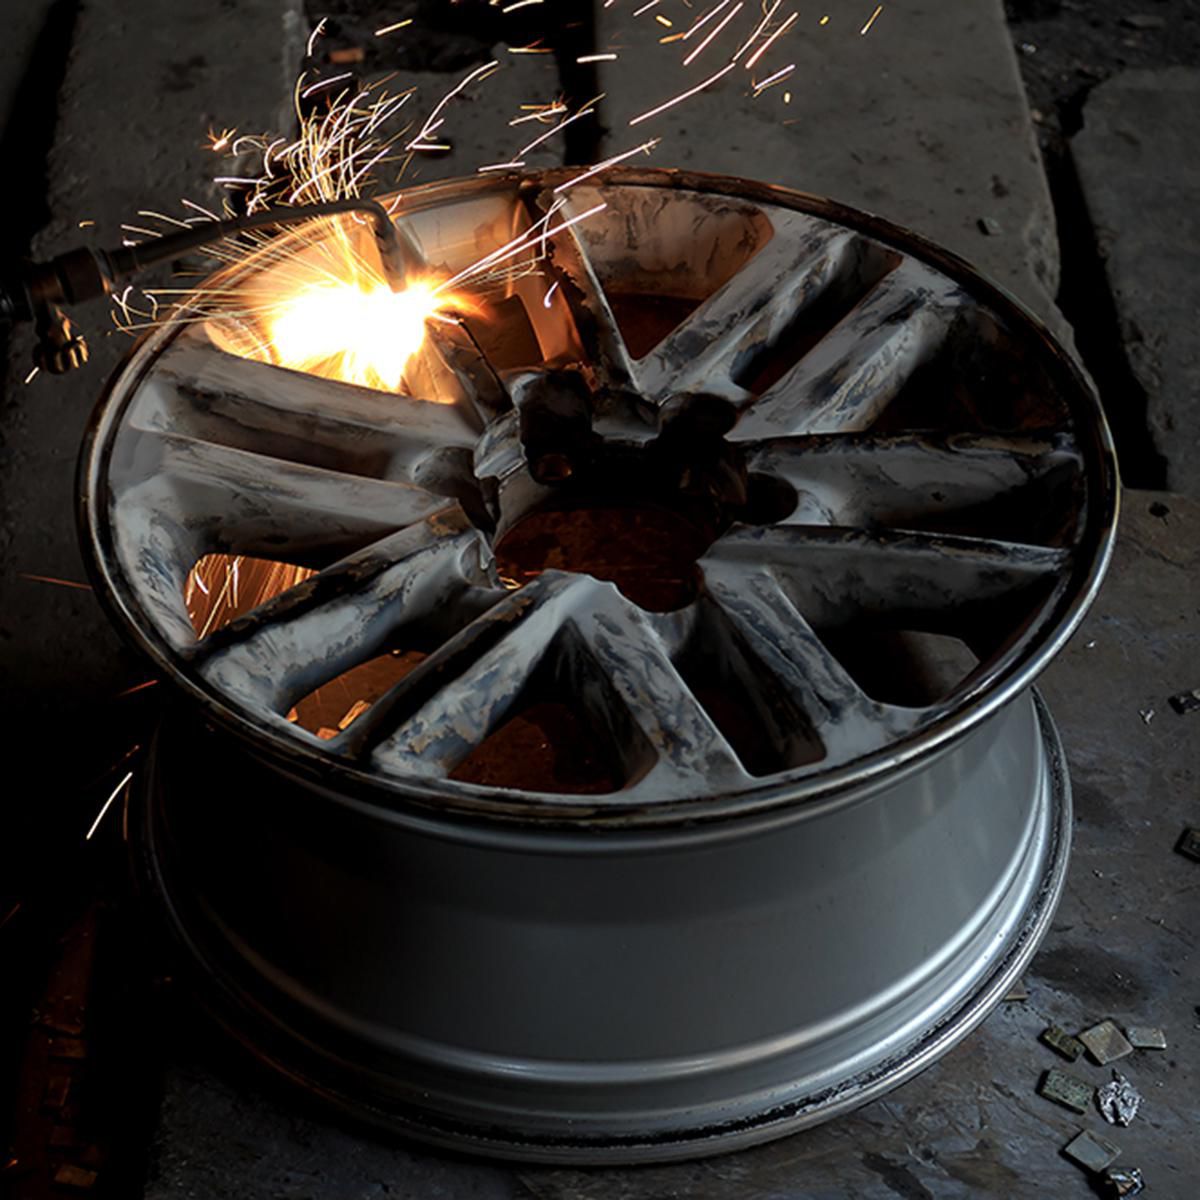
510 Aluminum Stick Rod Electrode, Flux Coated, 55 to 80 Amps, DCRP Polarity, Good Corrosion Resistance, Stable, Quiet Arc, 3/32"
(Pack of
2)
SKU:CW1826 Item#: CW1826
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.
Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: DC Reverse
Usage ProcedureMaintain the shortest arc possible, using DC reverse polarity only. On large heavy sections, preheating to 400°F (204°C) will produce faster, flatter deposit with no splatter. Electrode should be held almost perpendicular and use a rapid stringer or weaving technique with a backwhip at the crater. Bevel pieces 75° on sections 1/8" (3.2mm) or thicker.
Frequently Bought Together

510 Aluminum MIG Welding Wire 0.035"
$0.00
Couldn't load pickup availability
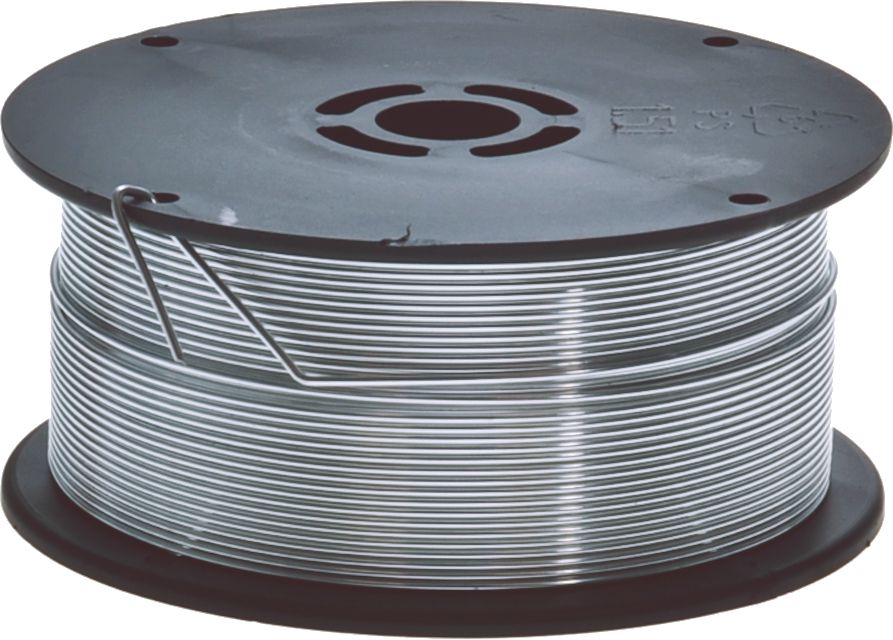
ER5356 Aluminum MIG Welding Wire 0.035"
$0.00
Couldn't load pickup availability
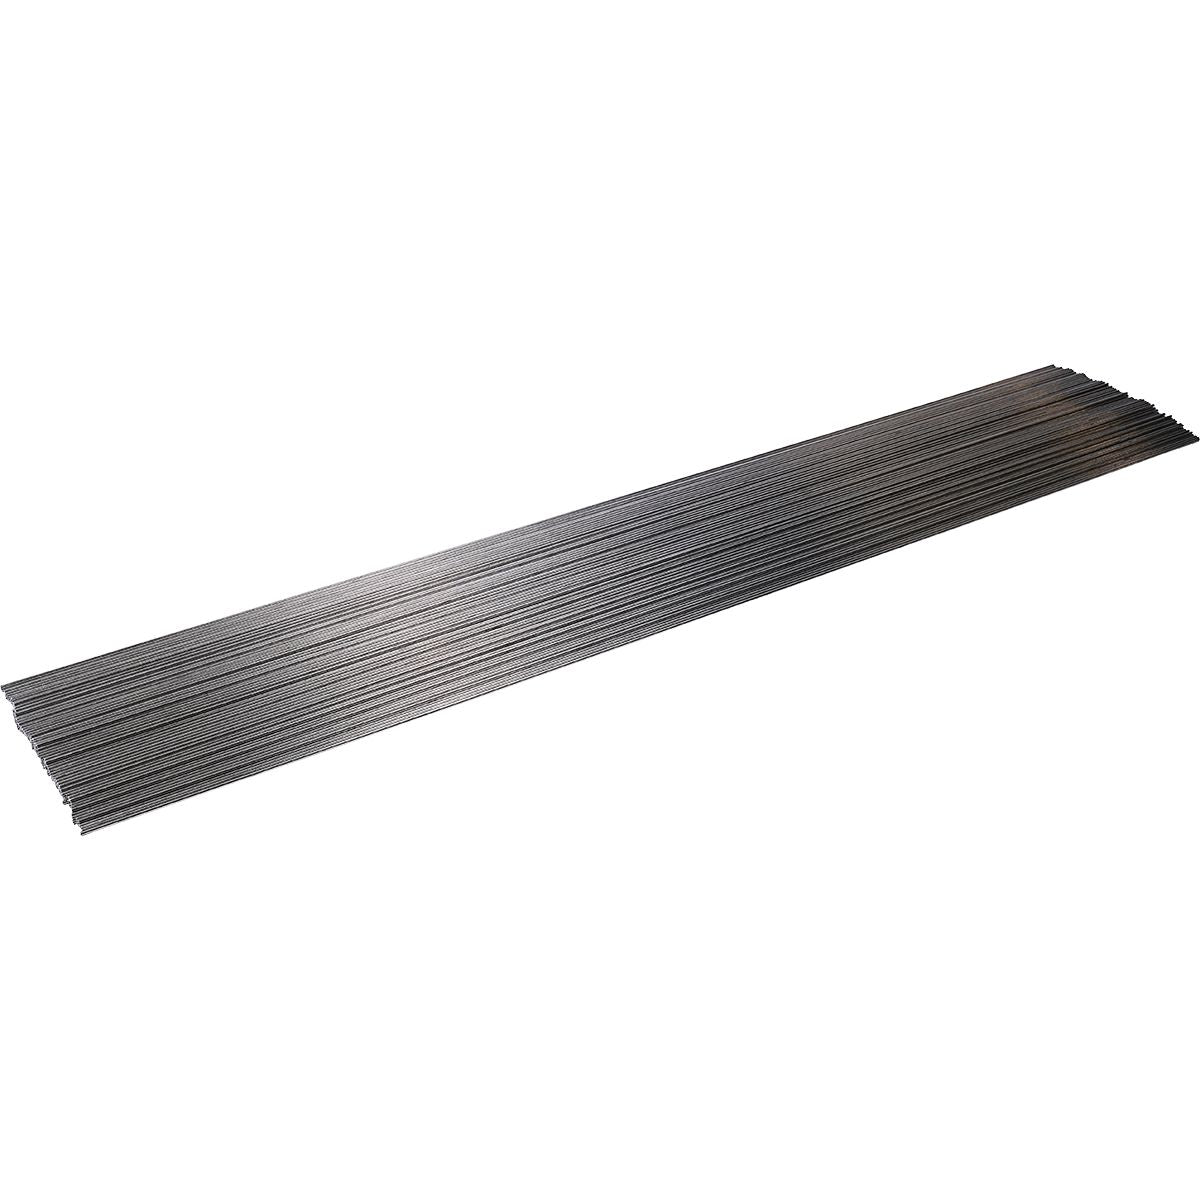
241T Aluminum Solid Tig Wire 3/32X36
$0.00
Couldn't load pickup availability
Front Fender Push-Type Retainer Nylon 18mm
$0.00
Couldn't load pickup availability
Rocker Molding Clip with Sealer Nylon Blue 17mm
$0.00
Couldn't load pickup availability

Fender and Bumper Push-Type Retainer Nylon 18mm
$0.00
Couldn't load pickup availability

TIG Torch FV-6 125A w/ Gas
$0.00
Couldn't load pickup availability

DC Welder Stick/TIG 15-200 A, 115-230V
$0.00
Couldn't load pickup availability

Hand Amp Control 12ft
$0.00
Couldn't load pickup availability

9-6506 Plasma Cutting Electrode
$0.00
Couldn't load pickup availability
Oxy-Therm Collet 3/8"
$0.00
Couldn't load pickup availability
Oxy-Therm Collet Grommet 1/4"
$0.00
Couldn't load pickup availability
Product Description
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: DC Reverse
Usage ProcedureMaintain the shortest arc possible, using DC reverse polarity only. On large heavy sections, preheating to 400°F (204°C) will produce faster, flatter deposit with no splatter. Electrode should be held almost perpendicular and use a rapid stringer or weaving technique with a backwhip at the crater. Bevel pieces 75° on sections 1/8" (3.2mm) or thicker.
Technical Specifications
| Item#: | CW1826 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 3/32 " |
| Tensile Strength | 35,000 PSI |
| Base Metal | Aluminum |
| Polarity | DCRP |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 2.0 lb |