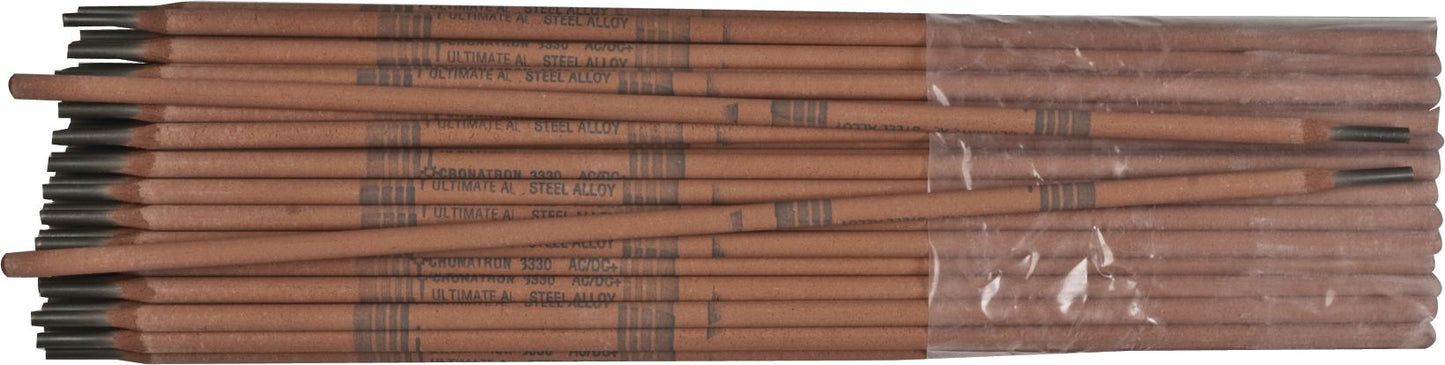
3330 Dissimilar Steel Stick Rod Electrode, Flux Coated, 100 to 145 Amps, 35% Elongation, DCRP/AC Polarity, 5/32"
(Pack of
5)
SKU:CW1872 Item#: CW1872
High-strength, dissimilar steel joining. Excels in out-of-position applications. Vertical-up and overhead.
Exceptional out-of-position welding
Tensile Strength: 127,000 PSI
Elongation: 37%
Hardness: 235 BHN
Polarity: AC or DC Reverse
Usage ProcedureUse AC or DC reverse polarity. Electrode may be used in a contact “drag” fashion or by holding a short arc. Stringer beads or a slight weave is best. Remove slag between passes. When welding alloyed or tool steel, preheat according to base metal requirements. For vertical-up welding, use a 1/8" electrode at approximately 65 to 70 amps or a 5/32" electrode at 75 to 85 amps. Use a weave “ledge” technique, pausing momentarily at end of weaves.
Couldn't load pickup availability
California Proposition 65: WARNING: Cancer and Reproductive Harm -
www.P65Warnings.ca.gov
Frequently Bought Together

333 Dissimilar Steel Stick Rod Electrode 3/32"
$0.00
Couldn't load pickup availability

Cross-Over Socket Set, SAE, 1/2" Drive, 10pc
$0.00
Couldn't load pickup availability
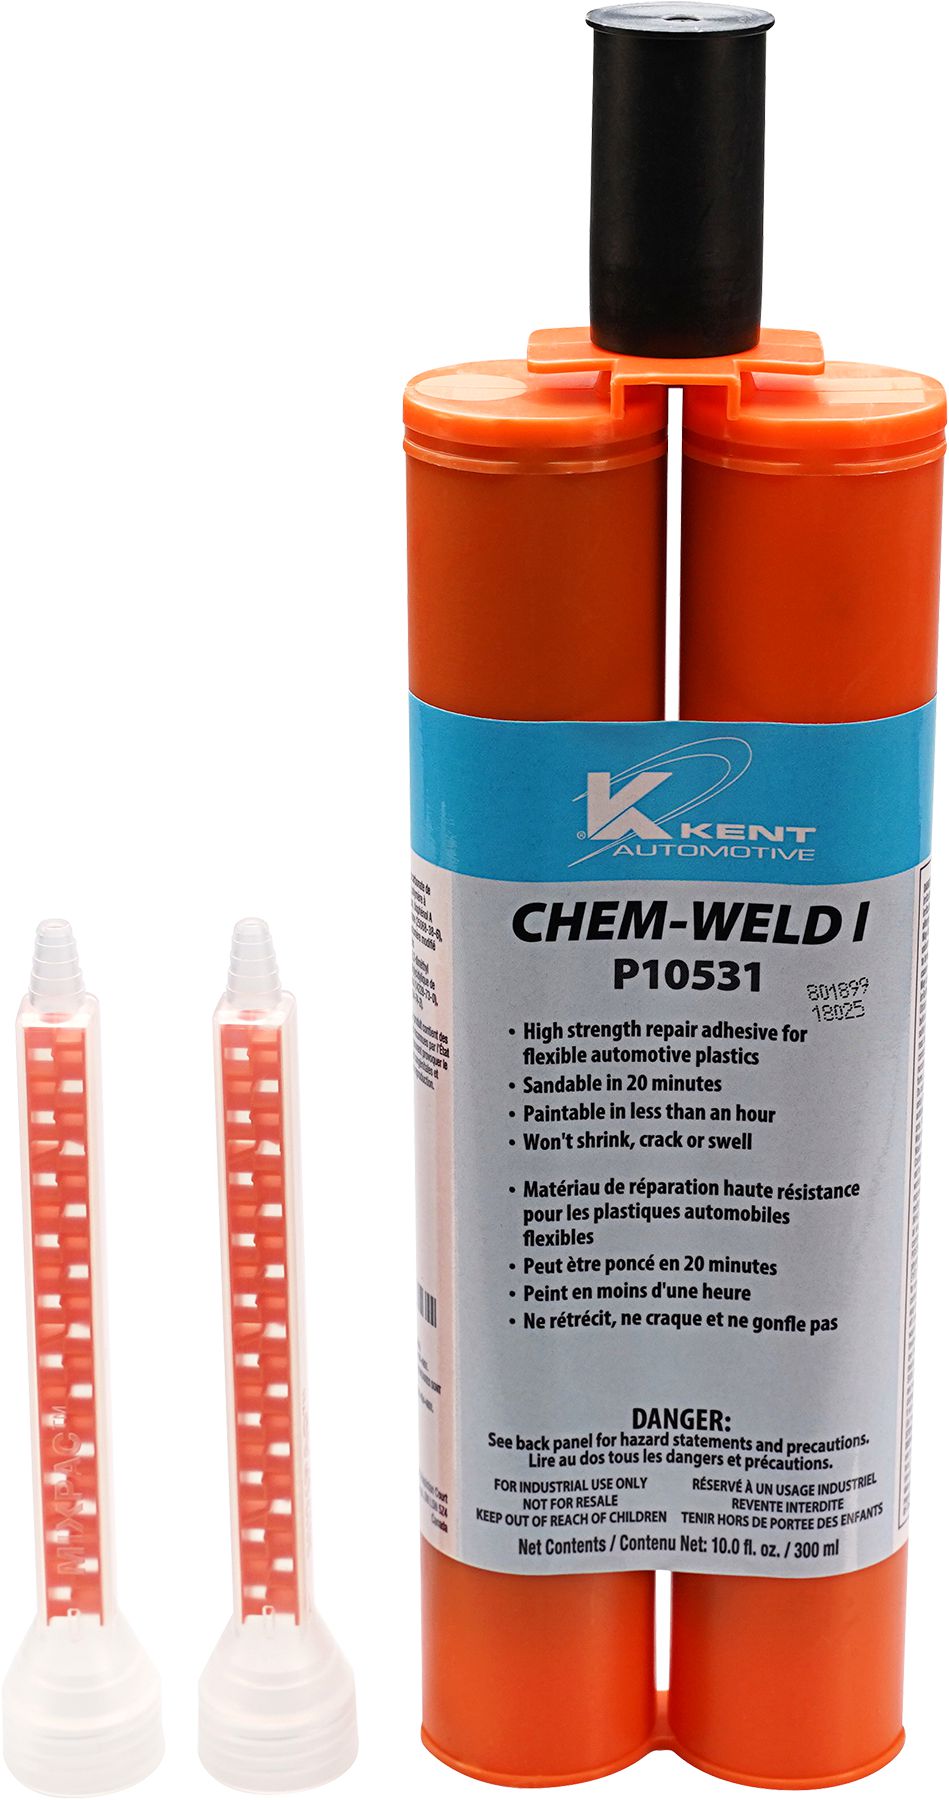
Chem-Weld I Plastic Repair Adhesive Black 10fl.oz
$0.00
Couldn't load pickup availability
Front Bumper Specialty Nut Steel M4.2-1.41
$0.00
Couldn't load pickup availability

Fender Apron Retainer Plastic 20mm
$0.00
Couldn't load pickup availability
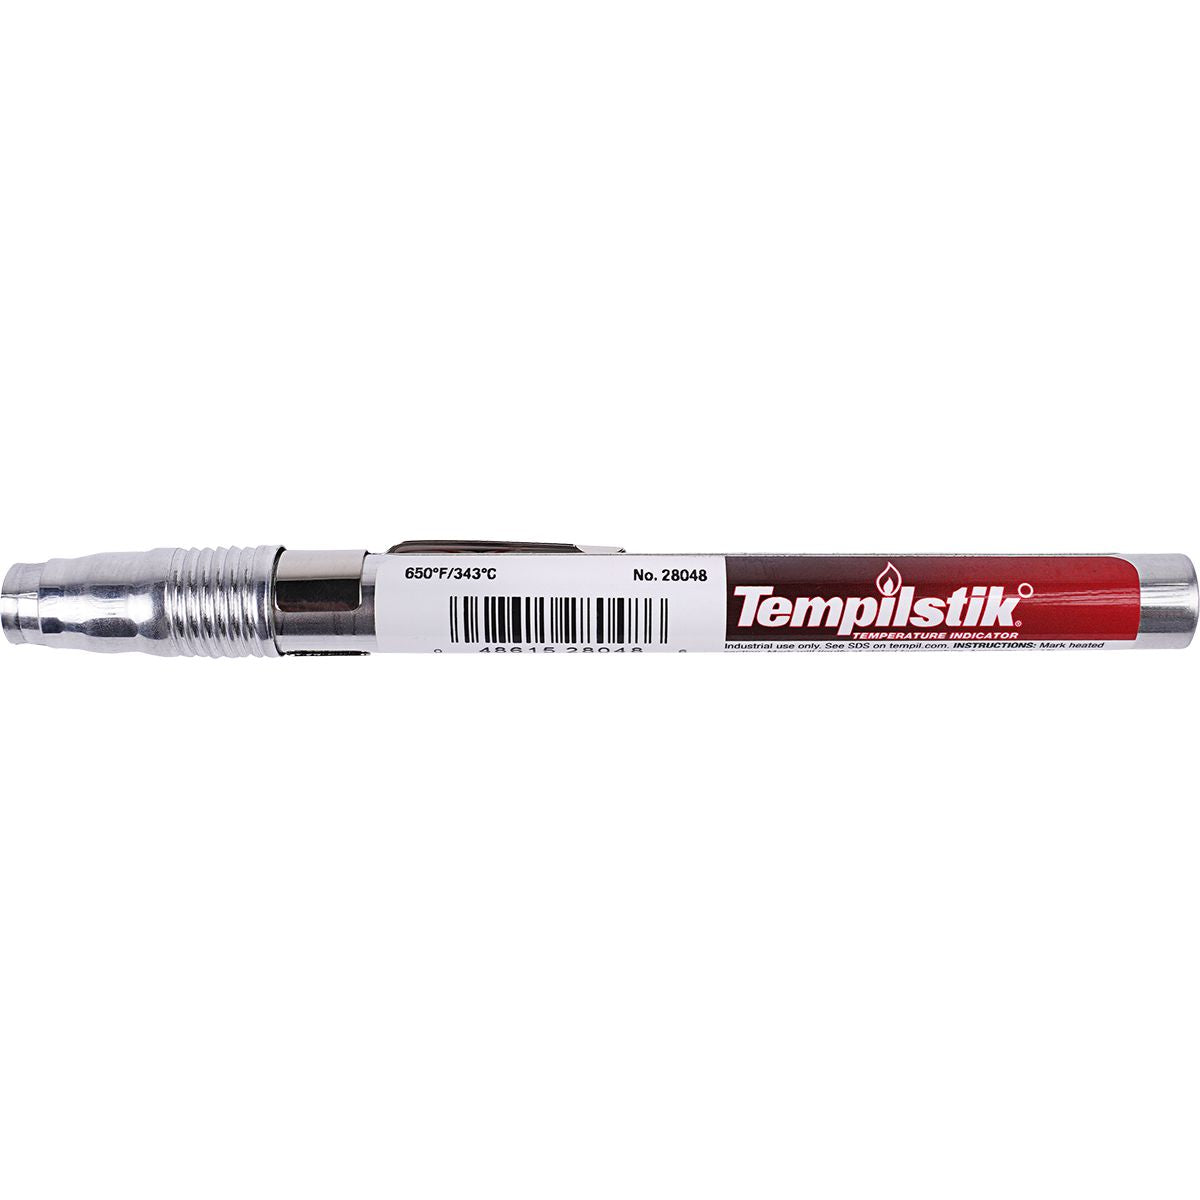
Heat Stick 850F Degrees
$0.00
Couldn't load pickup availability
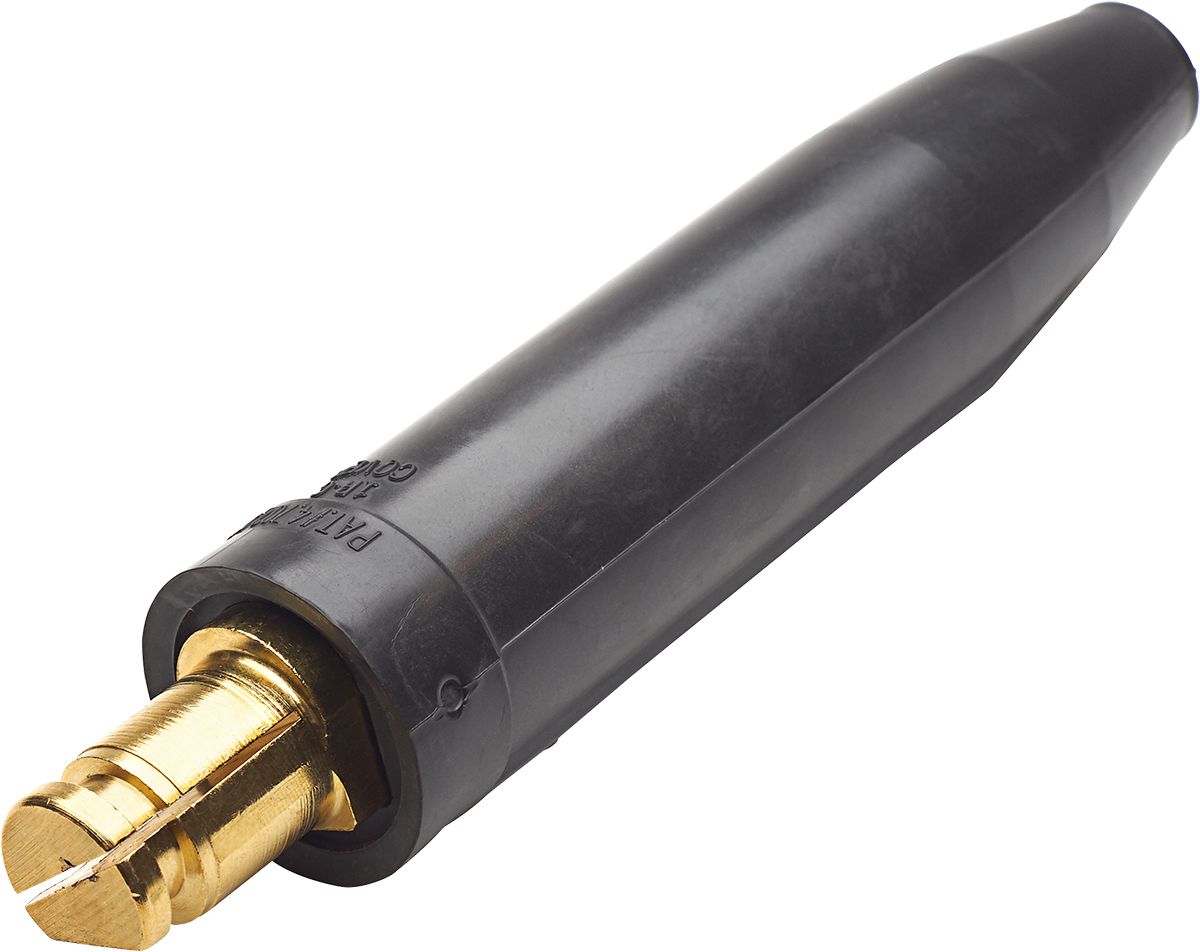
Cap Whip-Lead Connector #4 to #1
$0.00
Couldn't load pickup availability
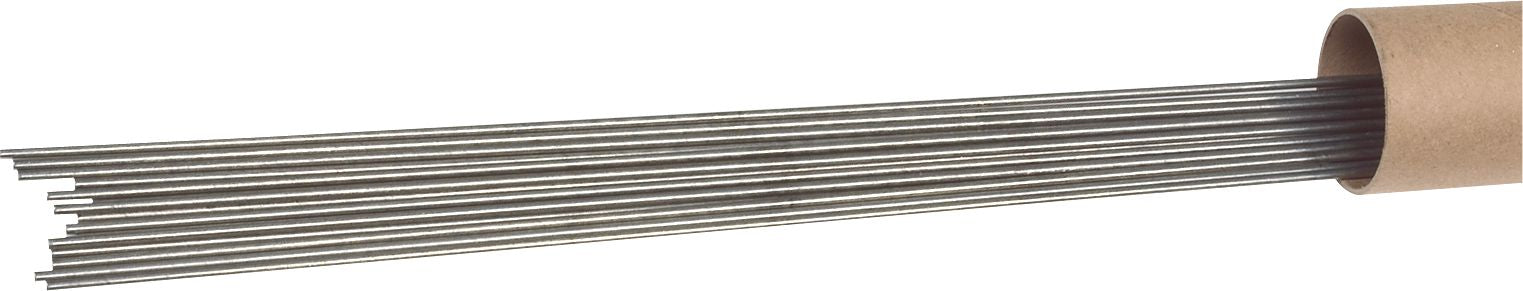
211 Cast Iron TIG Wire 1/8"
$0.00
Couldn't load pickup availability
Product Description
High-strength, dissimilar steel joining. Excels in out-of-position applications. Vertical-up and overhead.Exceptional out-of-position welding
Tensile Strength: 127,000 PSI
Elongation: 37%
Hardness: 235 BHN
Polarity: AC or DC Reverse
Usage ProcedureUse AC or DC reverse polarity. Electrode may be used in a contact “drag” fashion or by holding a short arc. Stringer beads or a slight weave is best. Remove slag between passes. When welding alloyed or tool steel, preheat according to base metal requirements. For vertical-up welding, use a 1/8" electrode at approximately 65 to 70 amps or a 5/32" electrode at 75 to 85 amps. Use a weave “ledge” technique, pausing momentarily at end of weaves.
Technical Specifications
| Item#: | CW1872 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 5/32 " |
| Tensile Strength | 125,000 PSI |
| Yield Strength | 100,000 PSI |
| Elongation | 35 % |
| Polarity | DCRP/AC |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 5.0 lb |
Product Restrictions
California Proposition 65: WARNING: Cancer and Reproductive Harm -
www.P65Warnings.ca.gov