3330 Dissimilar Steel Stick Rod Electrode, Flux Coated, 50 to 75 Amps, 35% Elongation, DCRP/AC Polarity, 3/32"
(Pack of
5)
SKU:CW1874 Item#: CW1874
High-strength, dissimilar steel joining. Excels in out-of-position applications. Vertical-up and overhead.
3330 Electrode – 3/32" Dia.
Specialty Alloy
High-Strength Alloy for Broken Stud Extraction
50A – 75A (DCRP/AC)
Overhead
Overhead Removal of All 1/4" and Over
Exceptional out-of-position welding
Tensile Strength: 127,000 PSI
Elongation: 37%
Hardness: 235 BHN
Polarity: AC or DC Reverse
Usage ProcedureUse AC or DC reverse polarity. Electrode may be used in a contact “drag” fashion or by holding a short arc. Stringer beads or a slight weave is best. Remove slag between passes. When welding alloyed or tool steel, preheat according to base metal requirements. For vertical-up welding, use a 1/8" electrode at approximately 65 to 70 amps or a 5/32" electrode at 75 to 85 amps. Use a weave “ledge” technique, pausing momentarily at end of weaves.
Frequently Bought Together

X-Tractalloy Welding Electrode Non-Conductive Flux 1/8 3/32 1LB EA
$0.00
Couldn't load pickup availability
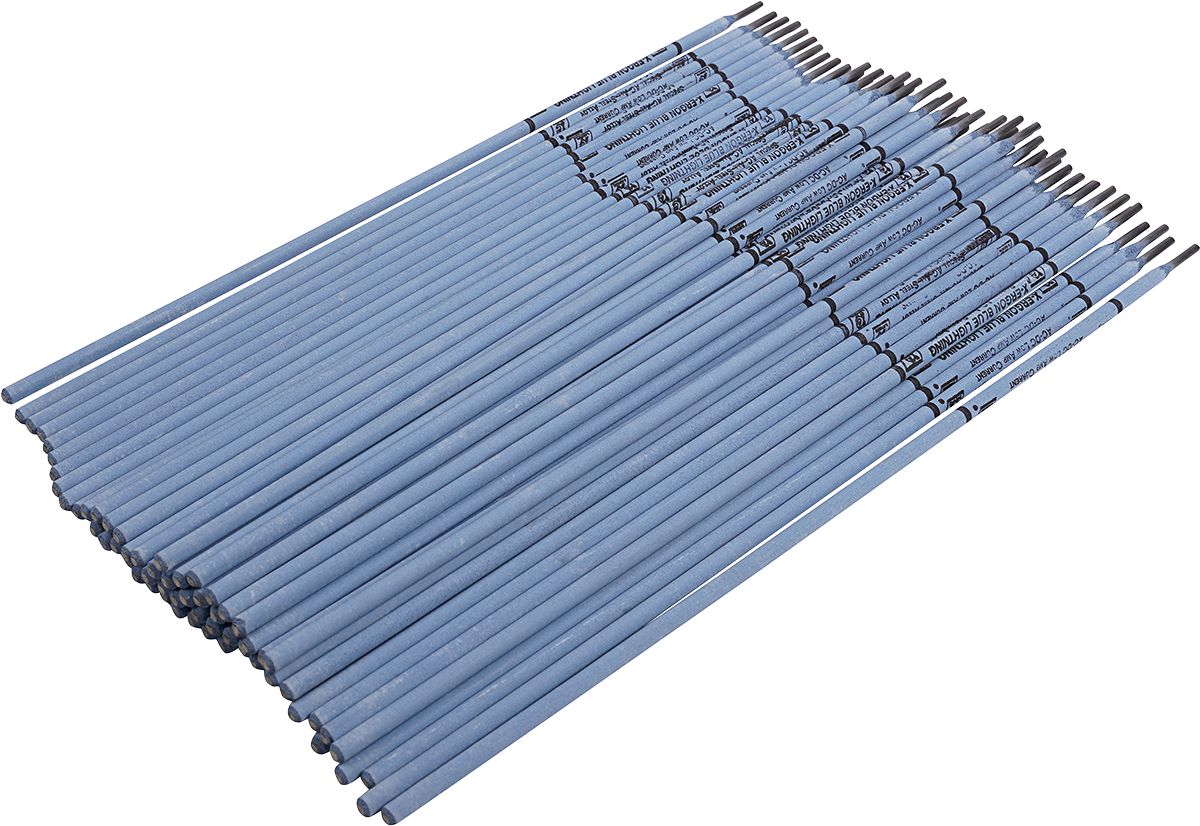
100 Blue Lightning Tough Duplex Alloy 5/32
$0.00
Couldn't load pickup availability

3330 Dissimilar Steel Stick Rod Electrode 5/32"
$0.00
Couldn't load pickup availability
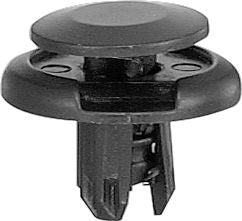
Front Fender Push-Type Retainer Nylon 20mm
$0.00
Couldn't load pickup availability
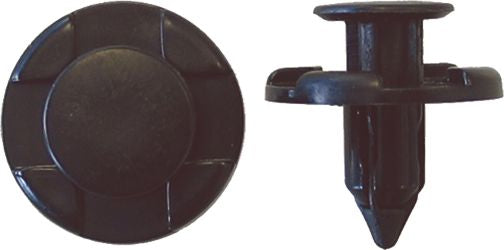
Front Bumper Drive Rivet Plastic 7mm Hole
$0.00
Couldn't load pickup availability
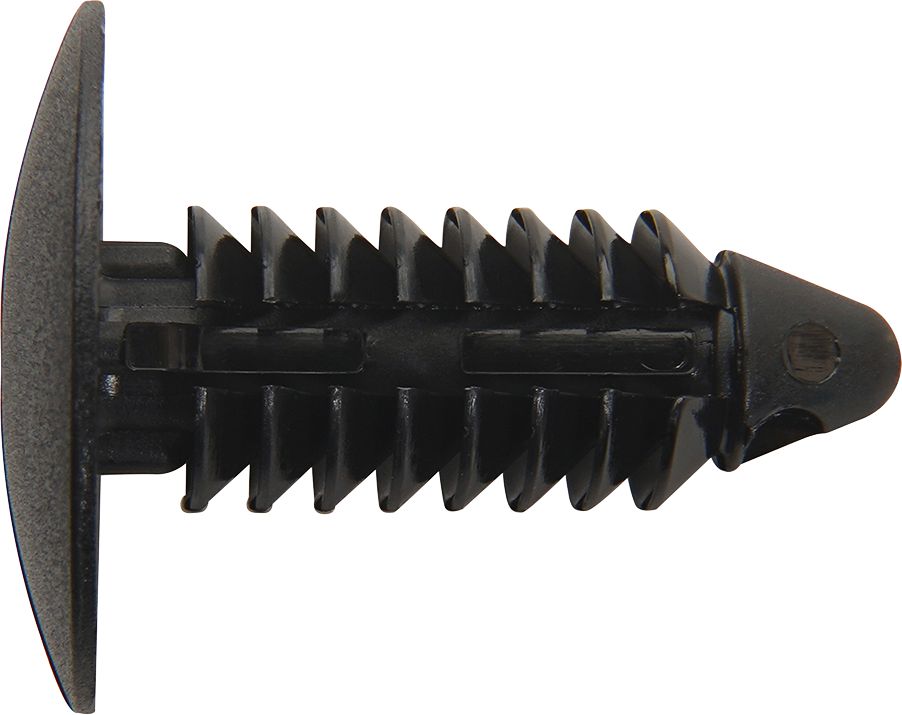
Fender Bumper Shield Retainer 11/16"
$0.00
Couldn't load pickup availability
Flint For Spring Loaded Trigger Torch Lighter
$0.00
Couldn't load pickup availability
Cronatron Welding Guide
$0.00
Couldn't load pickup availability
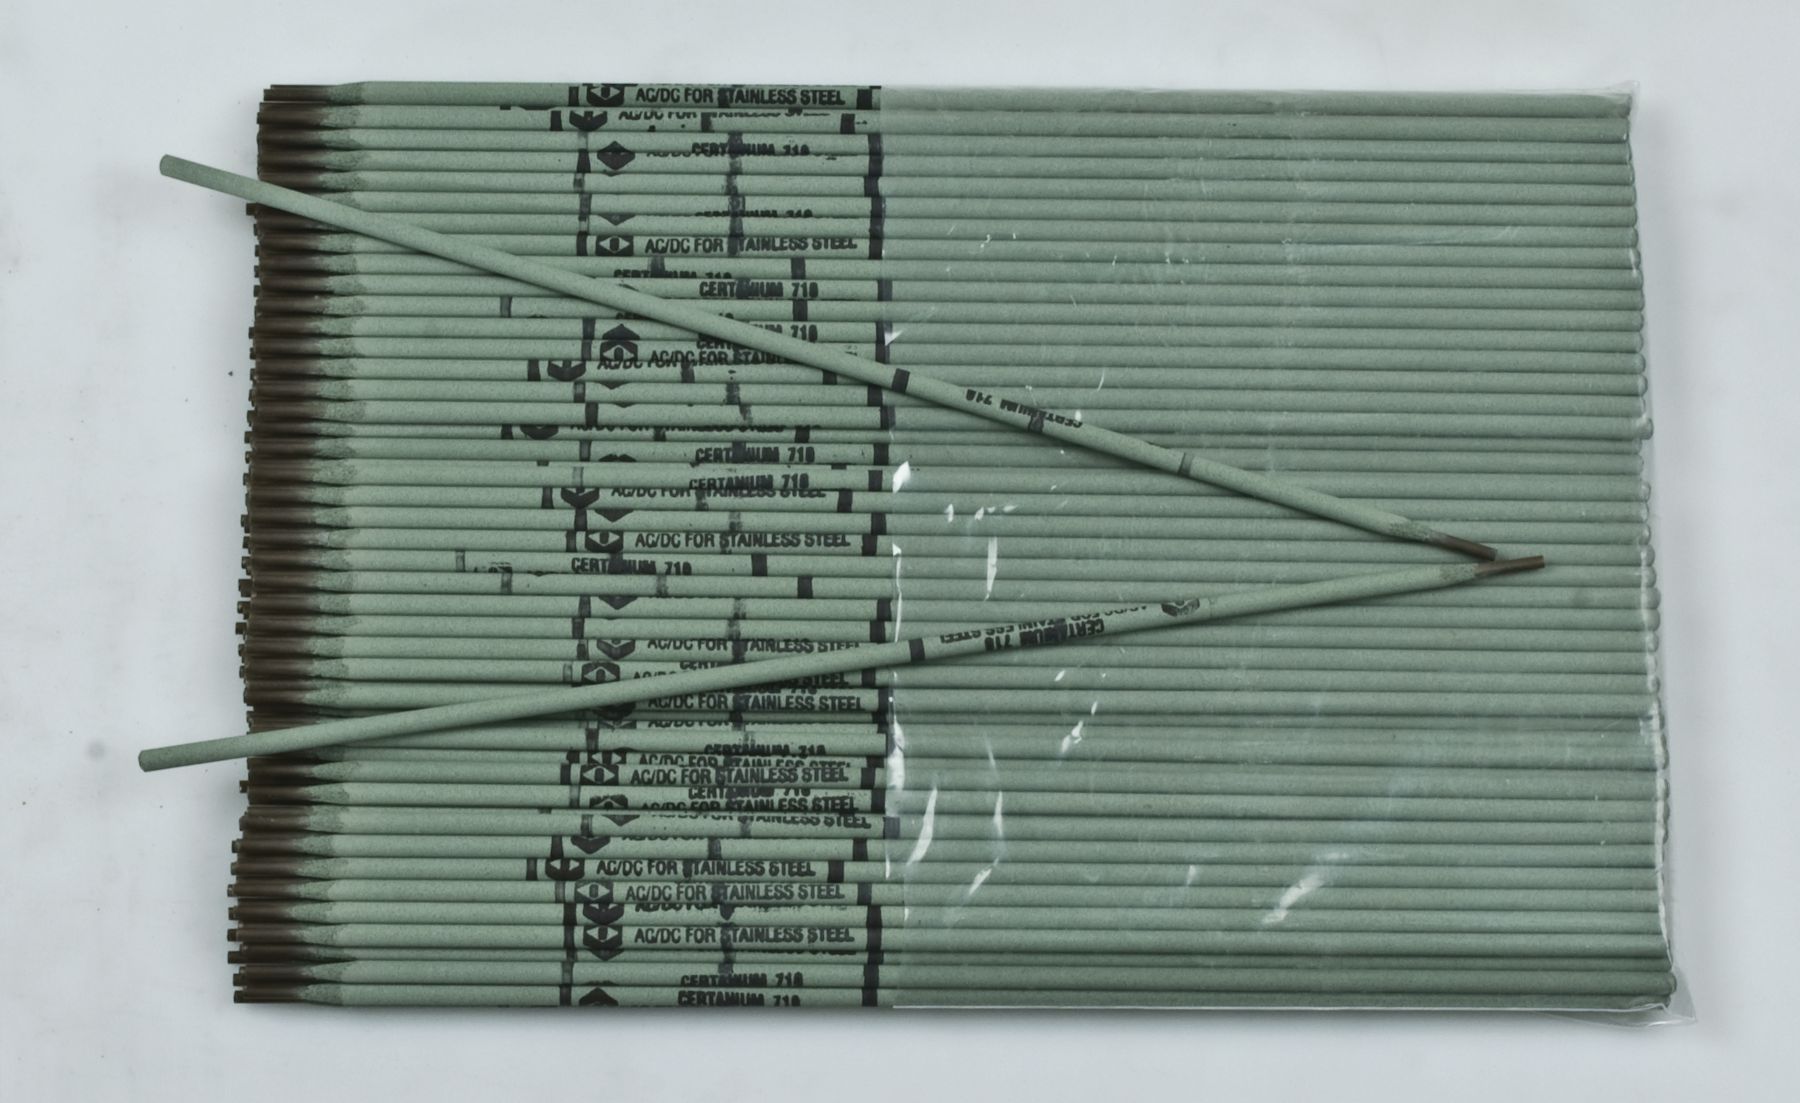
710 Stainless Steel Electrode 3/32"
$0.00
Couldn't load pickup availability

20463 Plasma Cutting Swirl Baffle
$0.00
Couldn't load pickup availability
177890 Plasma Cutting Tip
$0.00
Couldn't load pickup availability

8-7502 Plasma Cutting Electrode
$0.00
Couldn't load pickup availability
Product Description
High-strength, dissimilar steel joining. Excels in out-of-position applications. Vertical-up and overhead.3330 Electrode – 3/32" Dia.
Specialty Alloy
High-Strength Alloy for Broken Stud Extraction
50A – 75A (DCRP/AC)
Overhead
Overhead Removal of All 1/4" and Over
Exceptional out-of-position welding
Tensile Strength: 127,000 PSI
Elongation: 37%
Hardness: 235 BHN
Polarity: AC or DC Reverse
Usage ProcedureUse AC or DC reverse polarity. Electrode may be used in a contact “drag” fashion or by holding a short arc. Stringer beads or a slight weave is best. Remove slag between passes. When welding alloyed or tool steel, preheat according to base metal requirements. For vertical-up welding, use a 1/8" electrode at approximately 65 to 70 amps or a 5/32" electrode at 75 to 85 amps. Use a weave “ledge” technique, pausing momentarily at end of weaves.
Technical Specifications
| Item#: | CW1874 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 3/32 " |
| Tensile Strength | 125,000 PSI |
| Yield Strength | 100,000 PSI |
| Elongation | 35 % |
| Polarity | DCRP/AC |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 5.23 lb |
Product Restrictions