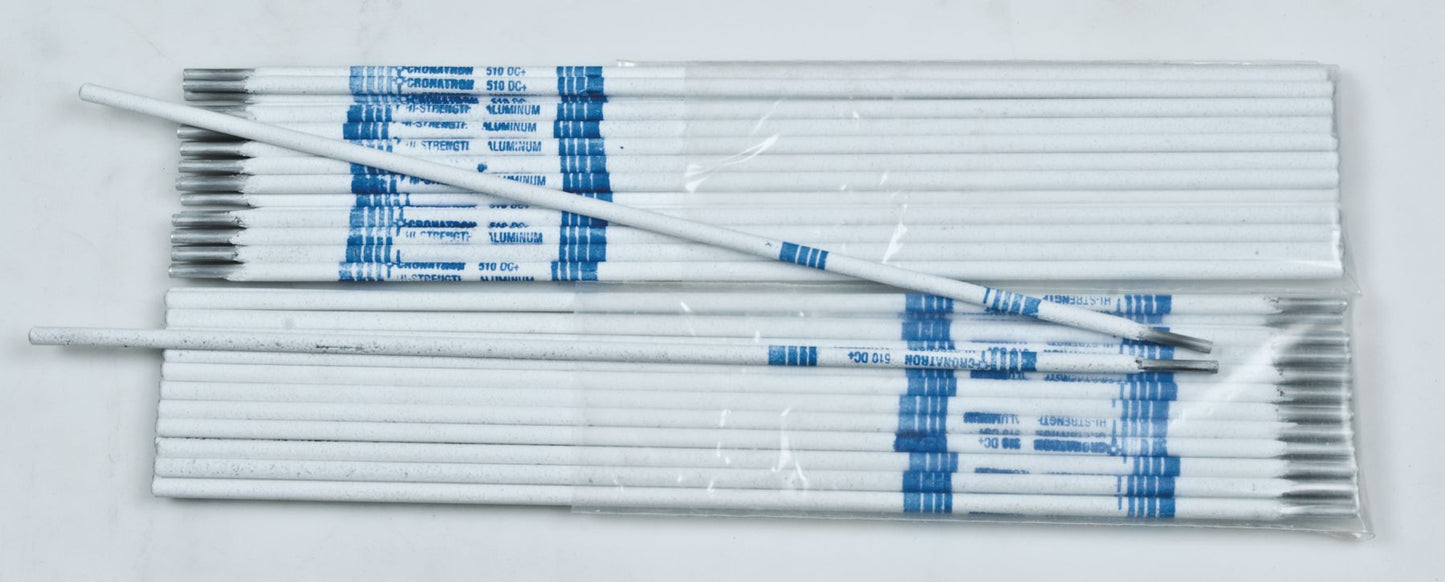
510 Aluminum Stick Rod Electrode, Flux Coated, 105 to 160 Amps, DCRP Polarity, Good Corrosion Resistance, Stable, Quiet Arc, 5/32"
(Pack of
2)
SKU:CW1038 Item#: CW1038
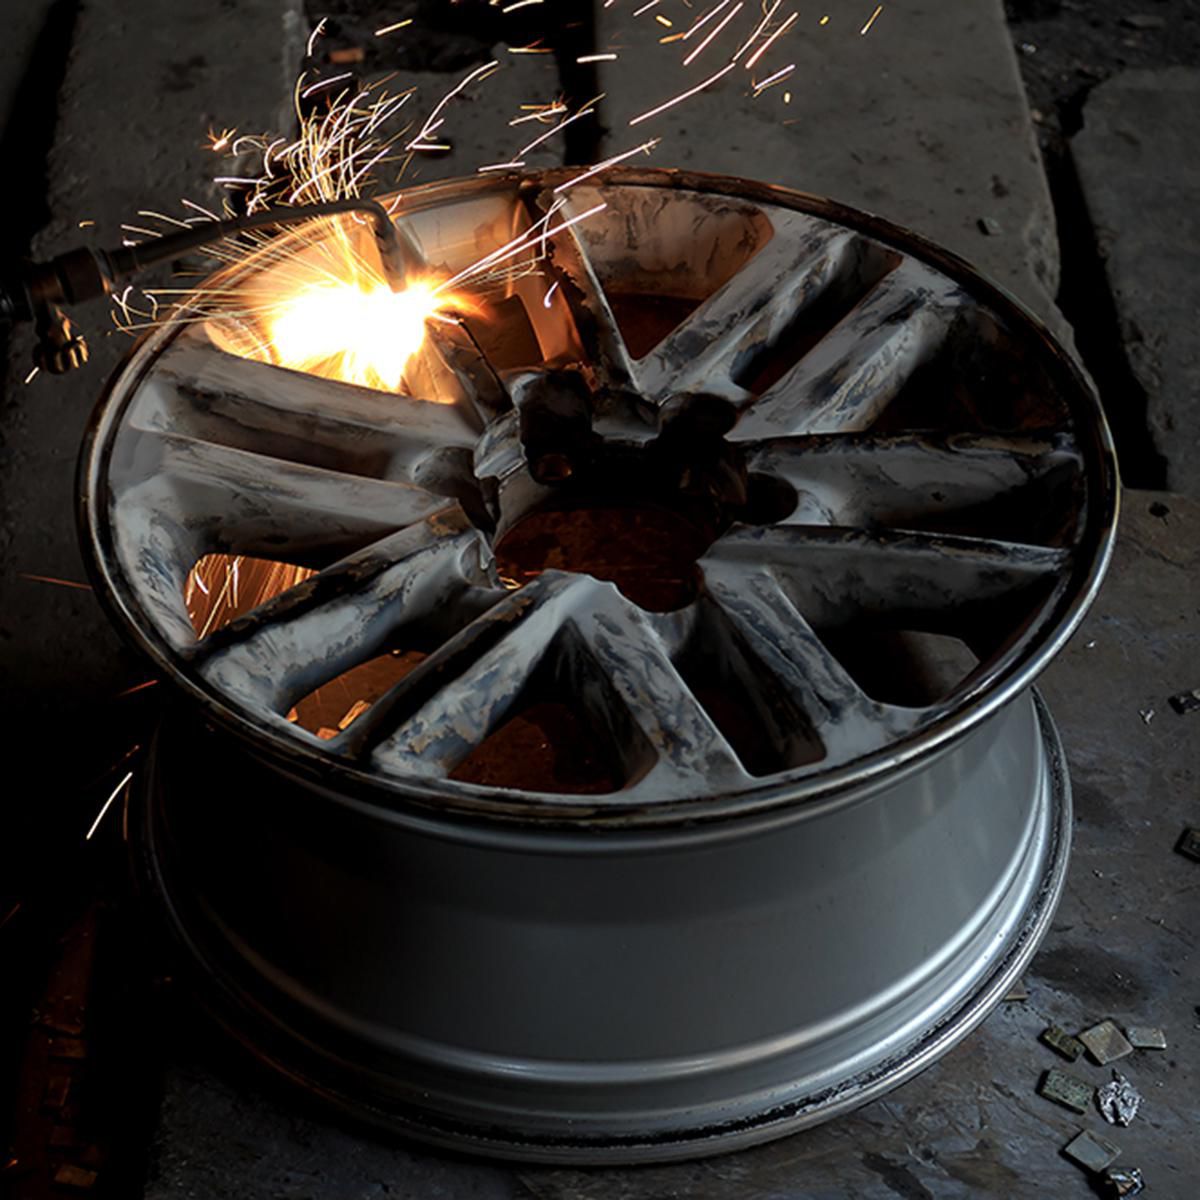
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.
Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: DC Reverse
Usage ProcedureMaintain the shortest arc possible, using DC reverse polarity only. On large heavy sections, preheating to 400°F (204°C) will produce faster, flatter deposit with no splatter. Electrode should be held almost perpendicular and use a rapid stringer or weaving technique with a backwhip at the crater. Bevel pieces 75° on sections 1/8" (3.2mm) or thicker.
Frequently Bought Together

ER4043 Aluminum TIG Wire 3/32"
$0.00
Couldn't load pickup availability

556 Aluminum MIG Welding Wire 0.035"
$0.00
Couldn't load pickup availability
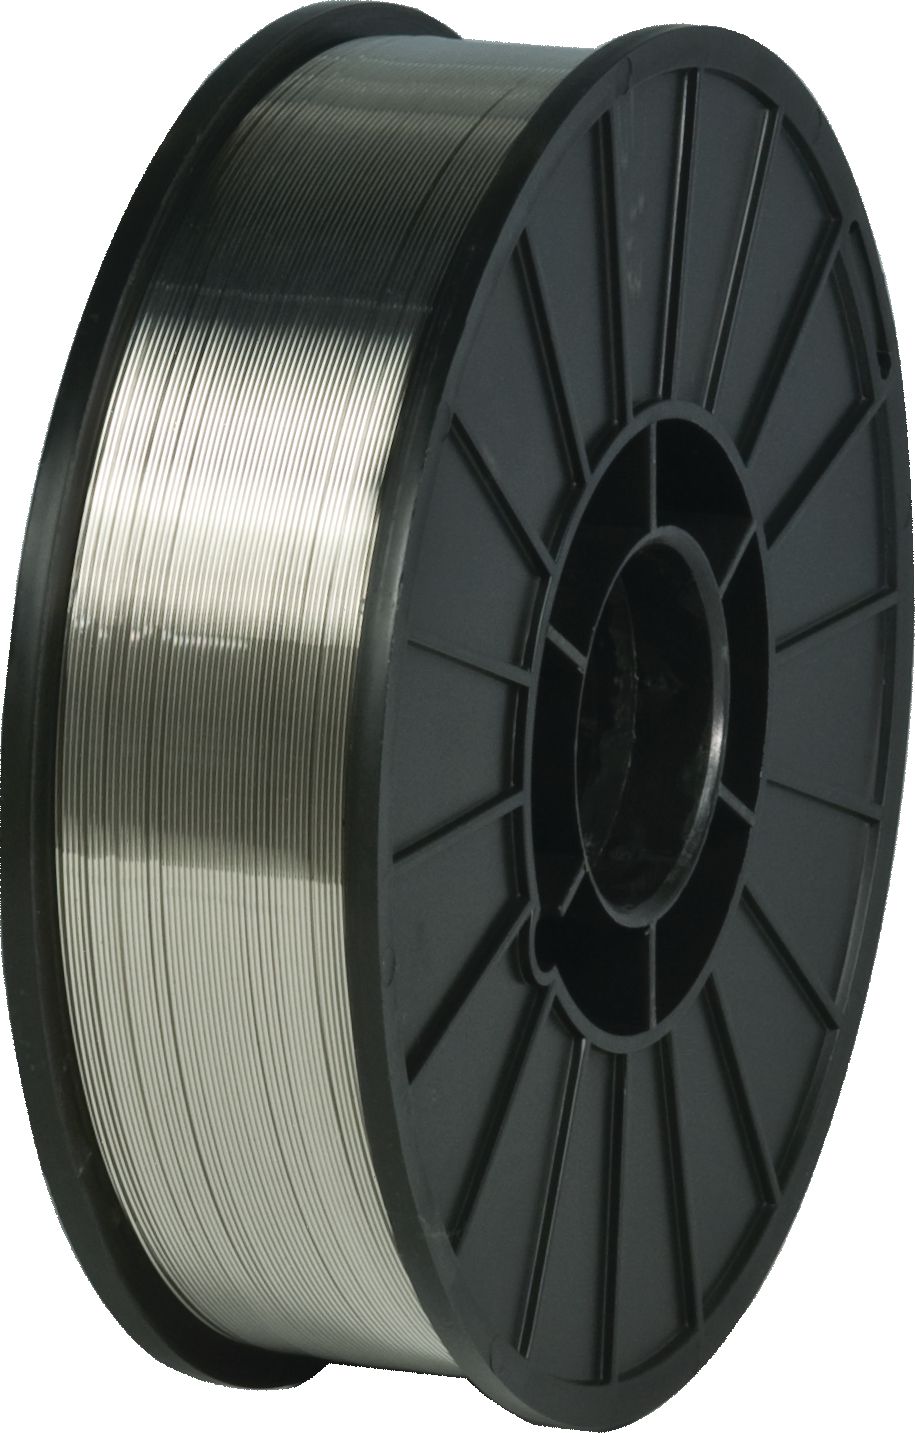
556 Aluminum MIG Welding Wire 0.035"
$0.00
Couldn't load pickup availability
Drive Rivet Nylon M8
$0.00
Couldn't load pickup availability
Bumper Push-Type Retainer Nylon 18mm
$0.00
Couldn't load pickup availability
Bumper Radiator and Grille Drive Rivet 7mm Hole
$0.00
Couldn't load pickup availability
Rosin Core Solder 0.032"
$0.00
Couldn't load pickup availability

Plastic Inside Corner No Wave Welder Staple
$0.00
Couldn't load pickup availability

Plastic Welder Staple Assortment 400Pcs
$0.00
Couldn't load pickup availability
606 Duraweld M Mig Wire Maintenance Grade Mild Steel Solid Mig Wire
$0.00
Couldn't load pickup availability

Er70S-6 Mild/Carbon Steel Mig Welding Wire 0.035
$0.00
Couldn't load pickup availability

CuSi-A Wire for Mig Brazing, 10lbs
$0.00
Couldn't load pickup availability
Product Description
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: DC Reverse
Usage ProcedureMaintain the shortest arc possible, using DC reverse polarity only. On large heavy sections, preheating to 400°F (204°C) will produce faster, flatter deposit with no splatter. Electrode should be held almost perpendicular and use a rapid stringer or weaving technique with a backwhip at the crater. Bevel pieces 75° on sections 1/8" (3.2mm) or thicker.
Technical Specifications
| Item#: | CW1038 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 5/32 " |
| Tensile Strength | 35,000 PSI |
| Base Metal | Aluminum |
| Polarity | DCRP |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 2.0 lb |