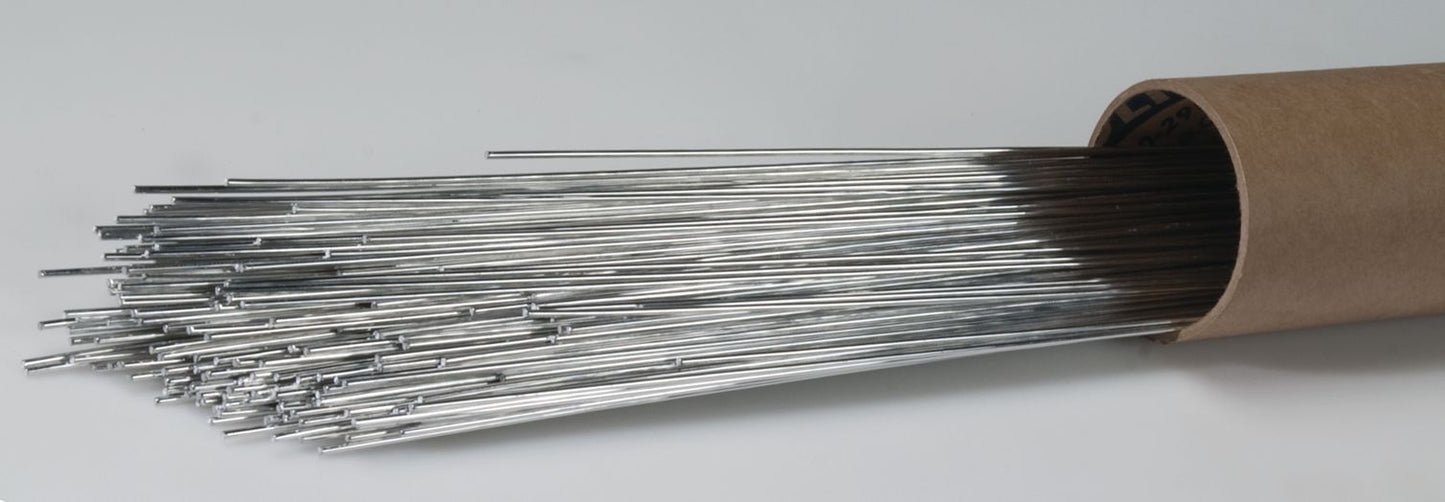
510 Aluminum TIG Wire, 100% Ar Shielding Gas, AC High Frequency Polarity, 36" Length, Quiet Arc, 1/16"
(Pack of
2)
SKU:CW1016 Item#: CW1016
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.
Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: AC/High Frequency
Gas: Argon/Helium
Usage ProcedureBevel heavy sections to allow 100% weld metal penetration. Sprinkle F56 flux into the joint area. Broadly heat area to be brazed with a large, soft and slightly carburizing flame to about 1,100°F (593°C). Heat the base metal until flux flows freely. The alloy will then begin to wet the base metal. Deposit the 510T to fill the joint. Flux residue may be removed with warm water and a brush.
Frequently Bought Together

641 Aluminum Solid Mig Wire .035X1LB
$0.00
Couldn't load pickup availability

ER4043 Aluminum TIG Wire 1/8"
$0.00
Couldn't load pickup availability
141 Aluminum Stick Electrode 5/32
$0.00
Couldn't load pickup availability
Front Bumper Push-Type Retainer Nylon 20mm
$0.00
Couldn't load pickup availability
Front Bumper and Radiator Support Drive Rivet
$0.00
Couldn't load pickup availability
Fender Bumper Shield Retainer 11/16"
$0.00
Couldn't load pickup availability
Flint For Spring Loaded Trigger Torch Lighter
$0.00
Couldn't load pickup availability
Cronatron Welding Guide
$0.00
Couldn't load pickup availability
710 Stainless Steel Electrode 3/32"
$0.00
Couldn't load pickup availability

8-7502 Plasma Cutting Electrode
$0.00
Couldn't load pickup availability
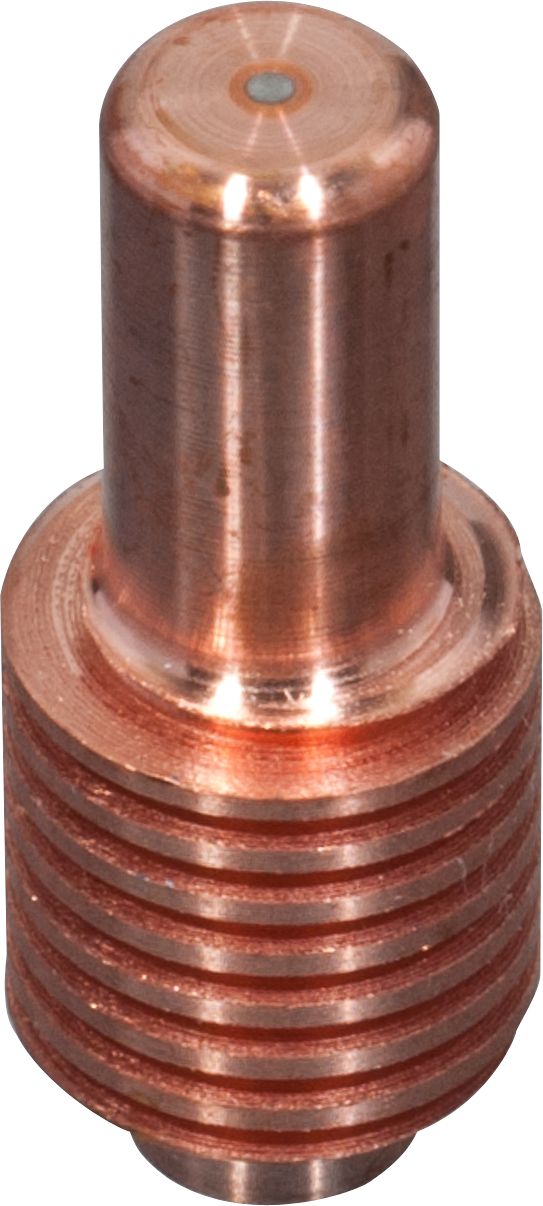
192047 Plasma Cutting Electrode
$0.00
Couldn't load pickup availability

8-7500 Plasma Cutting Shield Cup
$0.00
Couldn't load pickup availability
Product Description
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: AC/High Frequency
Gas: Argon/Helium
Usage ProcedureBevel heavy sections to allow 100% weld metal penetration. Sprinkle F56 flux into the joint area. Broadly heat area to be brazed with a large, soft and slightly carburizing flame to about 1,100°F (593°C). Heat the base metal until flux flows freely. The alloy will then begin to wet the base metal. Deposit the 510T to fill the joint. Flux residue may be removed with warm water and a brush.
Technical Specifications
| Item#: | CW1016 |
|---|---|
| Welding Process | TIG |
| Type | Solid |
| Diameter | 1/16 " |
| Length | 36 " |
| Tensile Strength | 35,000 PSI |
| Base Metal | Aluminum |
| Shielding Gas | 100% Ar |
| Polarity | AC High Freq |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 2.5 lb |