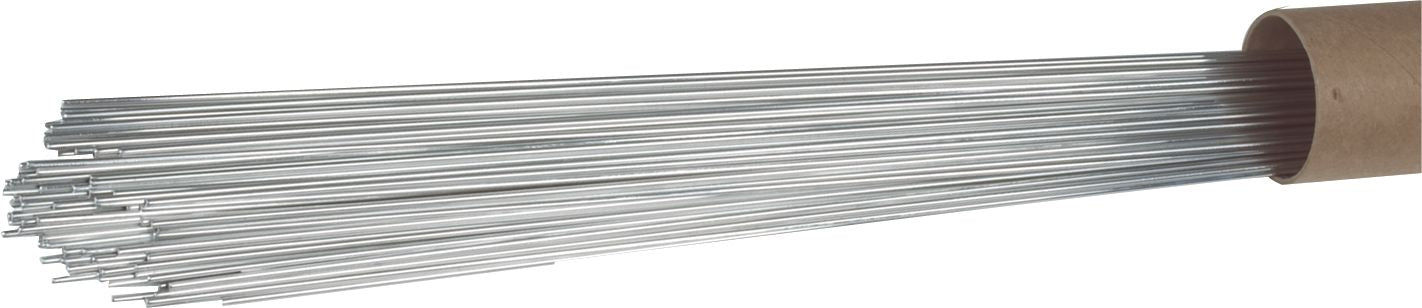
510 Aluminum TIG Wire, 100% Ar Shielding Gas, AC High Frequency Polarity, 36" Length, Quiet Arc, 3/32"
(Pack of
2)
SKU:CW1015 Item#: CW1015
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.
Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: AC/High Frequency
Gas: Argon/Helium
Usage ProcedureBevel heavy sections to allow 100% weld metal penetration. Sprinkle F56 flux into the joint area. Broadly heat area to be brazed with a large, soft and slightly carburizing flame to about 1,100°F (593°C). Heat the base metal until flux flows freely. The alloy will then begin to wet the base metal. Deposit the 510T to fill the joint. Flux residue may be removed with warm water and a brush.
Frequently Bought Together

ER5356 Aluminum TIG Wire 1/8"
$0.00
Couldn't load pickup availability

510 Aluminum MIG Welding Wire 0.035"
$0.00
Couldn't load pickup availability

ER5356 Aluminum MIG Welding Wire 0.0625"
$0.00
Couldn't load pickup availability
Bumper Fascia General Purpose Split Rivet 3/16"
$0.00
Couldn't load pickup availability
Fender Splash Shield Push Rivet Nylon 7mm Hole
$0.00
Couldn't load pickup availability
Specialty Rivet with Plastic Cap Aluminum 3.2mm
$0.00
Couldn't load pickup availability

Plastic Outside Corner No Wave Welder Staple
$0.00
Couldn't load pickup availability

Plastic Outside Corner Small Wave Welder Staple
$0.00
Couldn't load pickup availability

106 Mild Steel All Purpose Electrode
$0.00
Couldn't load pickup availability
AWS E71T-11 Carbon Steel MIG Flux Core Welding Wire .062" 33lb
$0.00
Couldn't load pickup availability
AWS E71T-11 Carbon Steel MIG Flux Core Welding Wire .035" 2lb
$0.00
Couldn't load pickup availability

9-6003 Plasma Cutting Shield Cup
$0.00
Couldn't load pickup availability
Product Description
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: AC/High Frequency
Gas: Argon/Helium
Usage ProcedureBevel heavy sections to allow 100% weld metal penetration. Sprinkle F56 flux into the joint area. Broadly heat area to be brazed with a large, soft and slightly carburizing flame to about 1,100°F (593°C). Heat the base metal until flux flows freely. The alloy will then begin to wet the base metal. Deposit the 510T to fill the joint. Flux residue may be removed with warm water and a brush.
Technical Specifications
| Item#: | CW1015 |
|---|---|
| Welding Process | TIG |
| Type | Solid |
| Diameter | 3/32 " |
| Length | 36 " |
| Tensile Strength | 35,000 PSI |
| Base Metal | Aluminum |
| Shielding Gas | 100% Ar |
| Polarity | AC High Freq |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 2.0 lb |