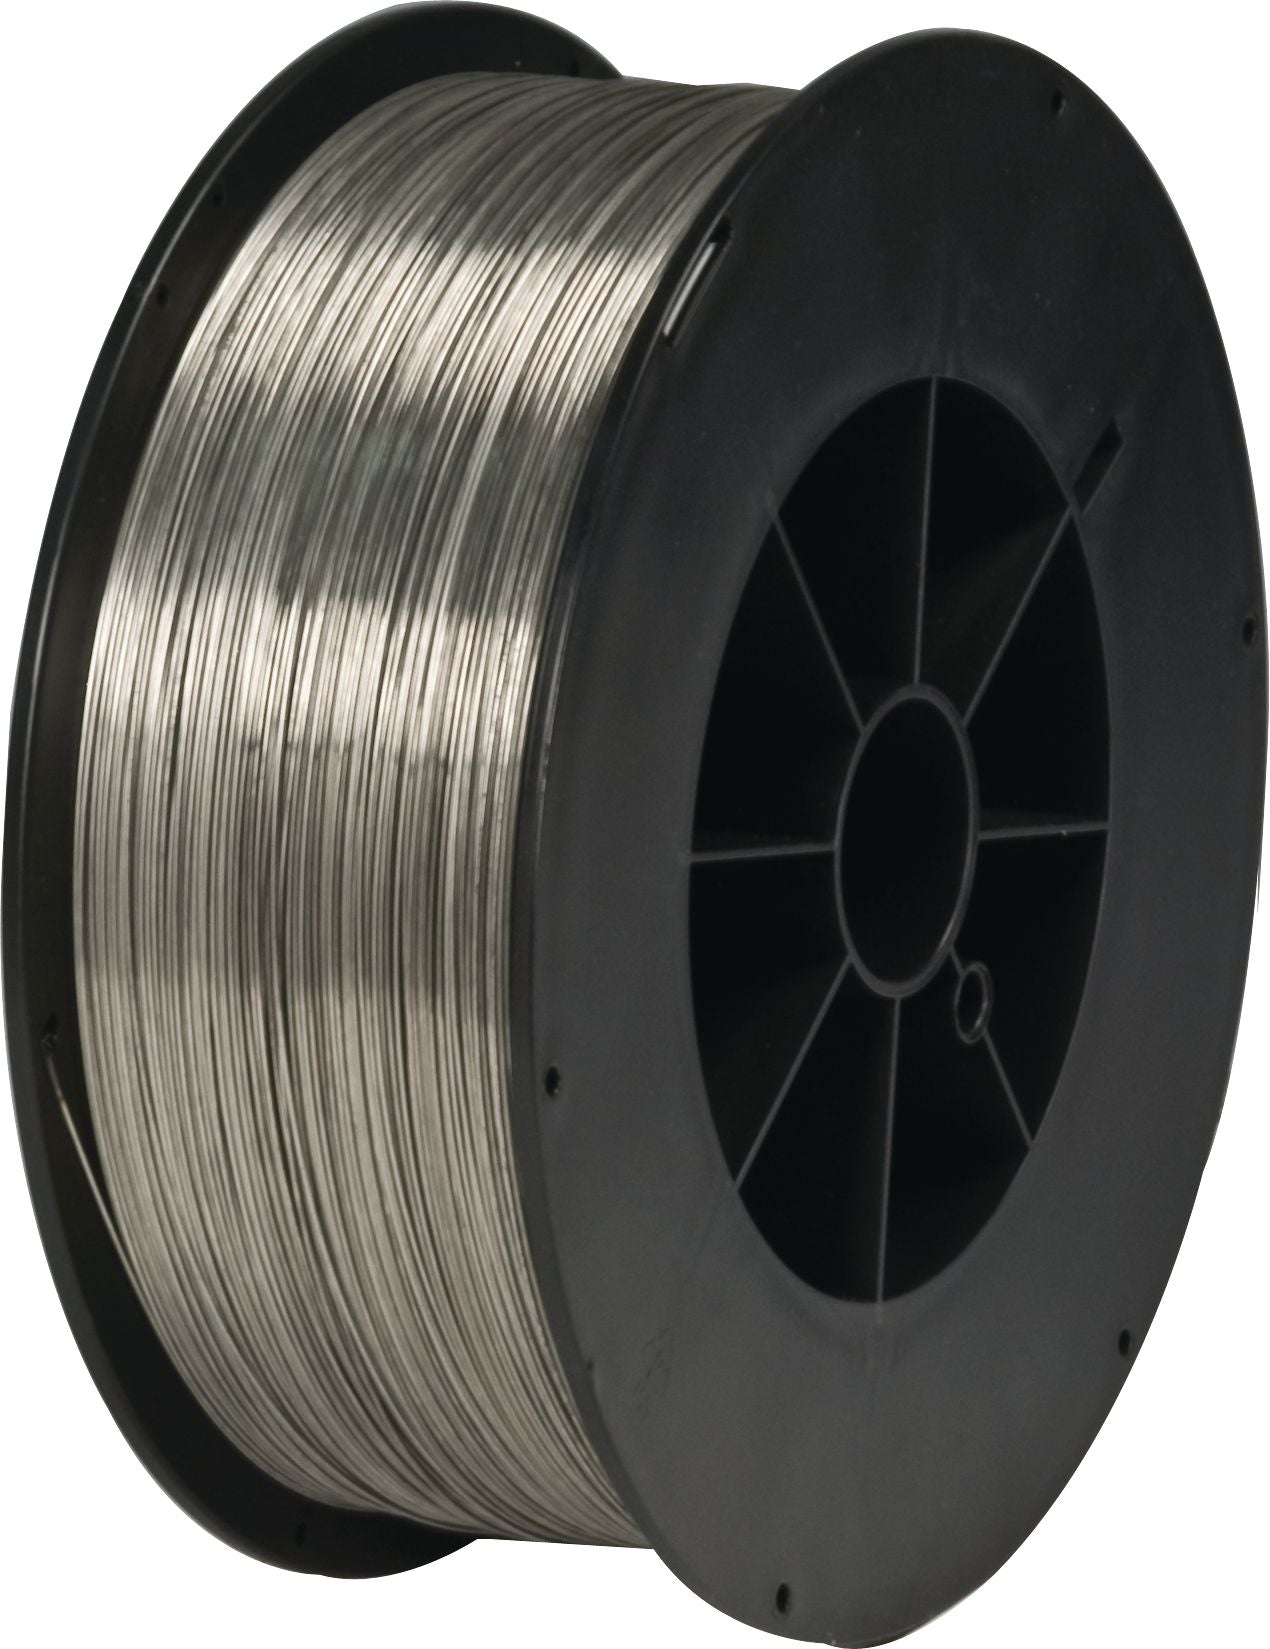
7310 Carbide Hard Facing MIG Welding Wire, Flux Cored, 52 to 57 HRC Hardness, DCRP Polarity, Good Edge Control, 1/16"
(Pack of
25)
SKU:CW1785 Item#: CW1785
Designed for high abrasion resistance in low to moderate impact situations.
Superior Advantages
• Minimal base metal dilution
• Maximum recovery (95% versus 65% typical)
• 1/4" dia. provides good out-of-position welding
• Good edge control
Hardness: Up to Rc 57 (3rd pass)
No. of Passes: Up to three
Polarity: DC Reverse
Gas: None or 75% Ar, 25% CO2
Chrome carbide alloy for severe abrasion and impact
Typical Applications
• Dredge pumps
• Screw conveyors
• Chutes for transporting sand and gravel
• Bucket lips
• Skid pads
Usage ProcedureWhen CRONALLOY EAGLE 7310 is applied via the open arc method, high deposition rates are possible.CRONALLOY EAGLE 7310 should be applied with DC reverse polarity for optimum arc stability.Refer to MIG Chart for operating parameters.
High Abrasion, Moderate Impact Resistance
Technical Tip:Individual applications will dictate correct welding procedures, but general rules should apply.Base metal should be free of rust, oil, scale, etc. before hardfacing is commenced. Spalled metal should be removed. On medium or high carbon steels, proper preheating procedures should be applied. Surface checking is normal in CRONALLOY EAGLE 7310, and where the possibility of crack propagation exists, a buffer layer should be applied prior to hardfacing.CRONALLOY EAGLE 7310 may be applied directly to carbon/low-alloy steels and austenitic manganese steels. Gray and ductile irons would require a buffer layer of CRONACAST™ 211. It should be noted that when welding on 11 – 14% manganese steel, the base metal must be kept cool (550°F/287°C). This can be accomplished by use of water sprays, air streams, or employing skip weld techniques. 11 – 14% manganese steel should be hardfaced via the open arc method.High alloy deposit is paramagnetic, cannot be flame-cut, forged or machined.
Frequently Bought Together
676 Flux Core Wire Extreme Abrasion Moderate Impact 1/16X33LBS
$0.00
Couldn't load pickup availability
281 Martensitic Hard Facing Welding Wire 0.045"
$0.00
Couldn't load pickup availability

178 Ultimate Abrasion Resistance 3/8X18IN
$0.00
Couldn't load pickup availability

174 Gray High Abrasion Moderate Impact 1/8
$0.00
Couldn't load pickup availability

7220 Carbide Hard Facing Stick Rod Electrode 3/8"
$0.00
Couldn't load pickup availability

Bumper Fascia Push-Type Retainer Nylon 18mm
$0.00
Couldn't load pickup availability
Fender Splash Shield Retainer Nylon 20mm
$0.00
Couldn't load pickup availability

Push-Type Retainer Nylon 15mm
$0.00
Couldn't load pickup availability
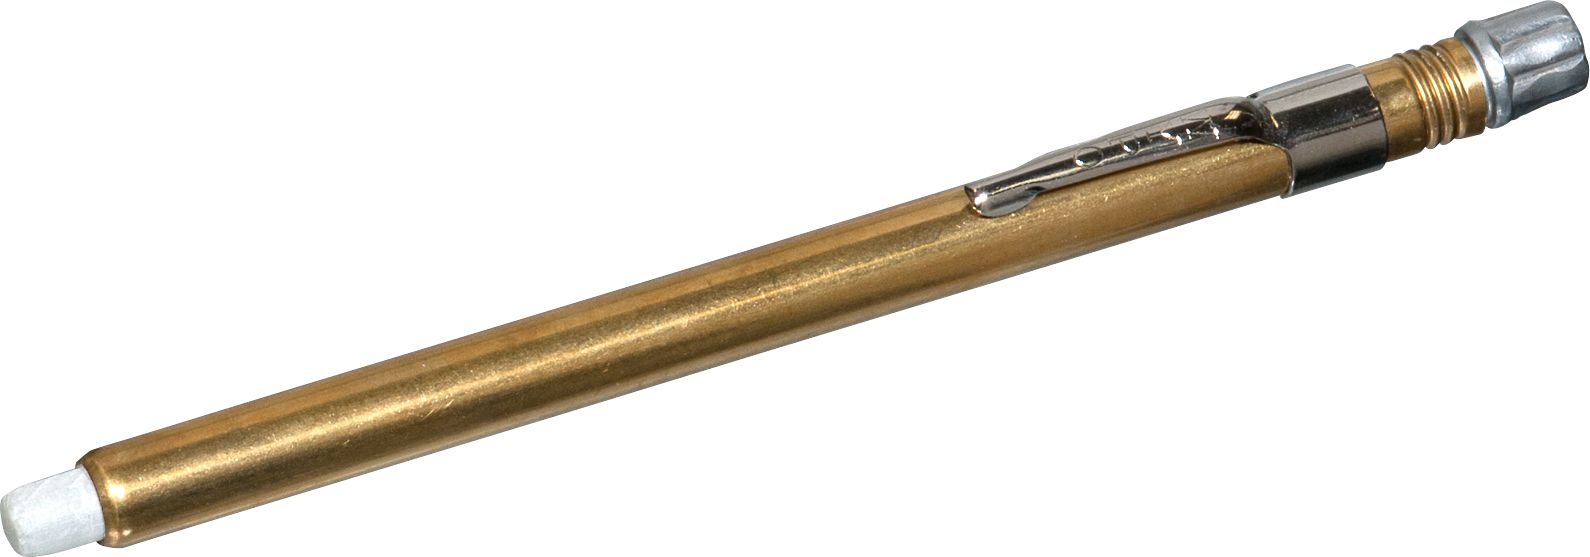
Round Soapstone Holder Heavy Duty
$0.00
Couldn't load pickup availability
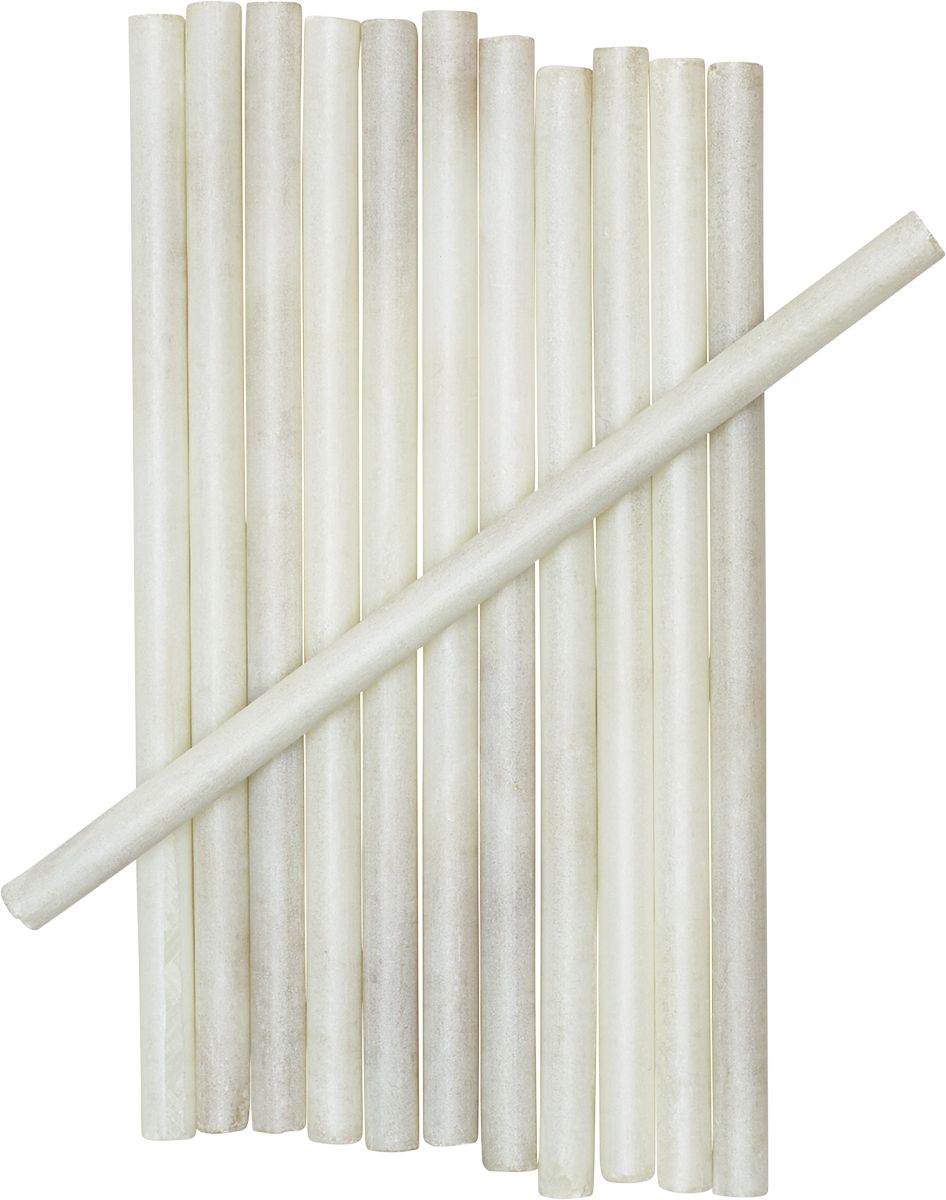
Round Soapstone 1/4 x 5"
$0.00
Couldn't load pickup availability
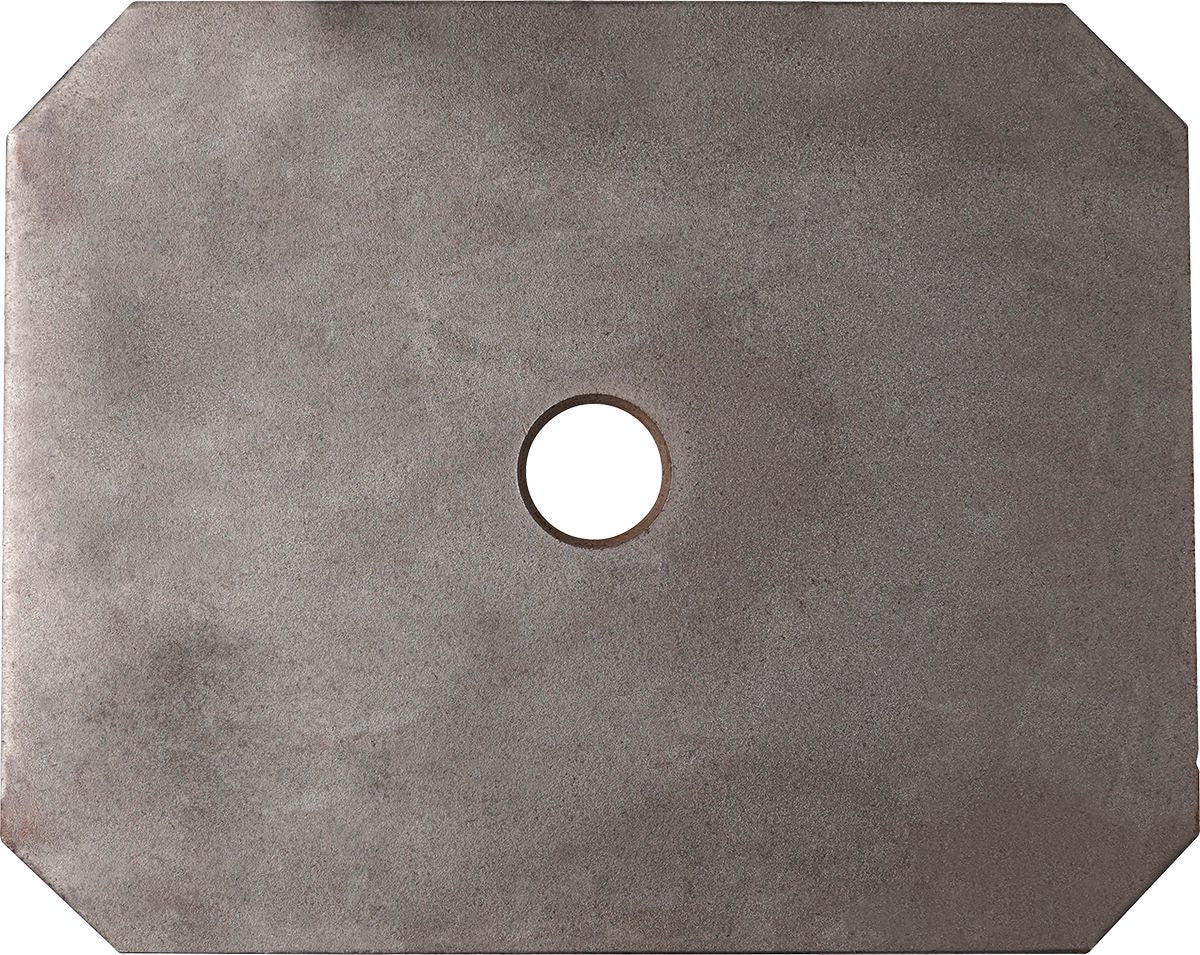
Wear Plates Used By Maintenance Welder 1/4X5X7
$0.00
Couldn't load pickup availability
Product Description
Designed for high abrasion resistance in low to moderate impact situations.Superior Advantages
• Minimal base metal dilution
• Maximum recovery (95% versus 65% typical)
• 1/4" dia. provides good out-of-position welding
• Good edge control
Hardness: Up to Rc 57 (3rd pass)
No. of Passes: Up to three
Polarity: DC Reverse
Gas: None or 75% Ar, 25% CO2
Chrome carbide alloy for severe abrasion and impact
Typical Applications
• Dredge pumps
• Screw conveyors
• Chutes for transporting sand and gravel
• Bucket lips
• Skid pads
Usage ProcedureWhen CRONALLOY EAGLE 7310 is applied via the open arc method, high deposition rates are possible.CRONALLOY EAGLE 7310 should be applied with DC reverse polarity for optimum arc stability.Refer to MIG Chart for operating parameters.
High Abrasion, Moderate Impact Resistance
Technical Tip:Individual applications will dictate correct welding procedures, but general rules should apply.Base metal should be free of rust, oil, scale, etc. before hardfacing is commenced. Spalled metal should be removed. On medium or high carbon steels, proper preheating procedures should be applied. Surface checking is normal in CRONALLOY EAGLE 7310, and where the possibility of crack propagation exists, a buffer layer should be applied prior to hardfacing.CRONALLOY EAGLE 7310 may be applied directly to carbon/low-alloy steels and austenitic manganese steels. Gray and ductile irons would require a buffer layer of CRONACAST™ 211. It should be noted that when welding on 11 – 14% manganese steel, the base metal must be kept cool (550°F/287°C). This can be accomplished by use of water sprays, air streams, or employing skip weld techniques. 11 – 14% manganese steel should be hardfaced via the open arc method.High alloy deposit is paramagnetic, cannot be flame-cut, forged or machined.
Technical Specifications
| Item#: | CW1785 |
|---|---|
| Welding Process | MIG |
| Type | Flux Cored |
| Diameter | 1/16 " |
| Base Metal | Carbide |
| Carbide Type | Chromium |
| Hardness | 52-57 HRC |
| Shielding Gas | No Gas |
| Polarity | DCRP |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 27.0 lb |
Product Restrictions