


53 Pot Metal Bare Brazing Rod, Shiny Grey, 18" Length, 1/8"
(Pack of
2)
SKU:CW1017 Item#: CW1017
Easily joins white and pot metals.
Superior Advantages
• Lead- and cadmium-free
• Extremely low melting point
• Two times stronger than ordinary solder
Low temperature, dissimilar pot metal
Tensile Strength: 17,500 PSI
Application Temperature: 360°F (182°C)
Recommended Flux: F53
Typical Applications
• Air conditioning and refrigeration units
• Brazing/soldering of copper to aluminum, brass to steel, stainless to zinc, etc.
Usage ProcedureBase metal must supply heat, as a direct flame is unworkable. A carburizing flame should be used. A flux is required for all applications where good bonding is desired.
Technical TipDo not direct torch at flux, as it will char. Allow CRONABRAZE 53 to solidify before quenching and removing flux residue. CRONASOLV™ F53 flux is recommended for all applications.
Frequently Bought Together
23 Copper and Steel Flux Coated Brazing Rod 1/8"
$0.00
Couldn't load pickup availability
30 Copper and Steel Flux Coated Brazing Rod 1/16"
$0.00
Couldn't load pickup availability
44 Silver Bare Brazing Rod 1/16"
$0.00
Couldn't load pickup availability
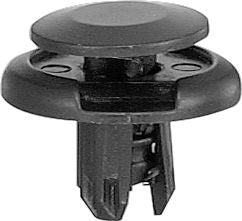
Front Bumper Drive Rivet Plastic 7mm Hole
$0.00
Couldn't load pickup availability
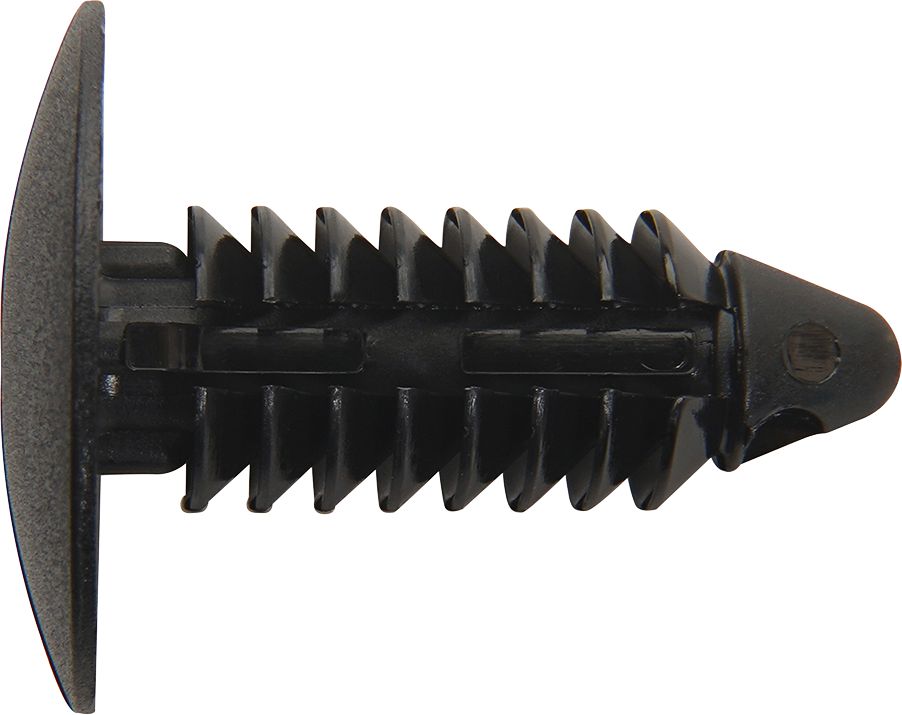
Front Fender Push-Type Retainer Nylon 20mm
$0.00
Couldn't load pickup availability
Fender Bumper Shield Retainer 11/16"
$0.00
Couldn't load pickup availability
Cronatron Welding Guide
$0.00
Couldn't load pickup availability
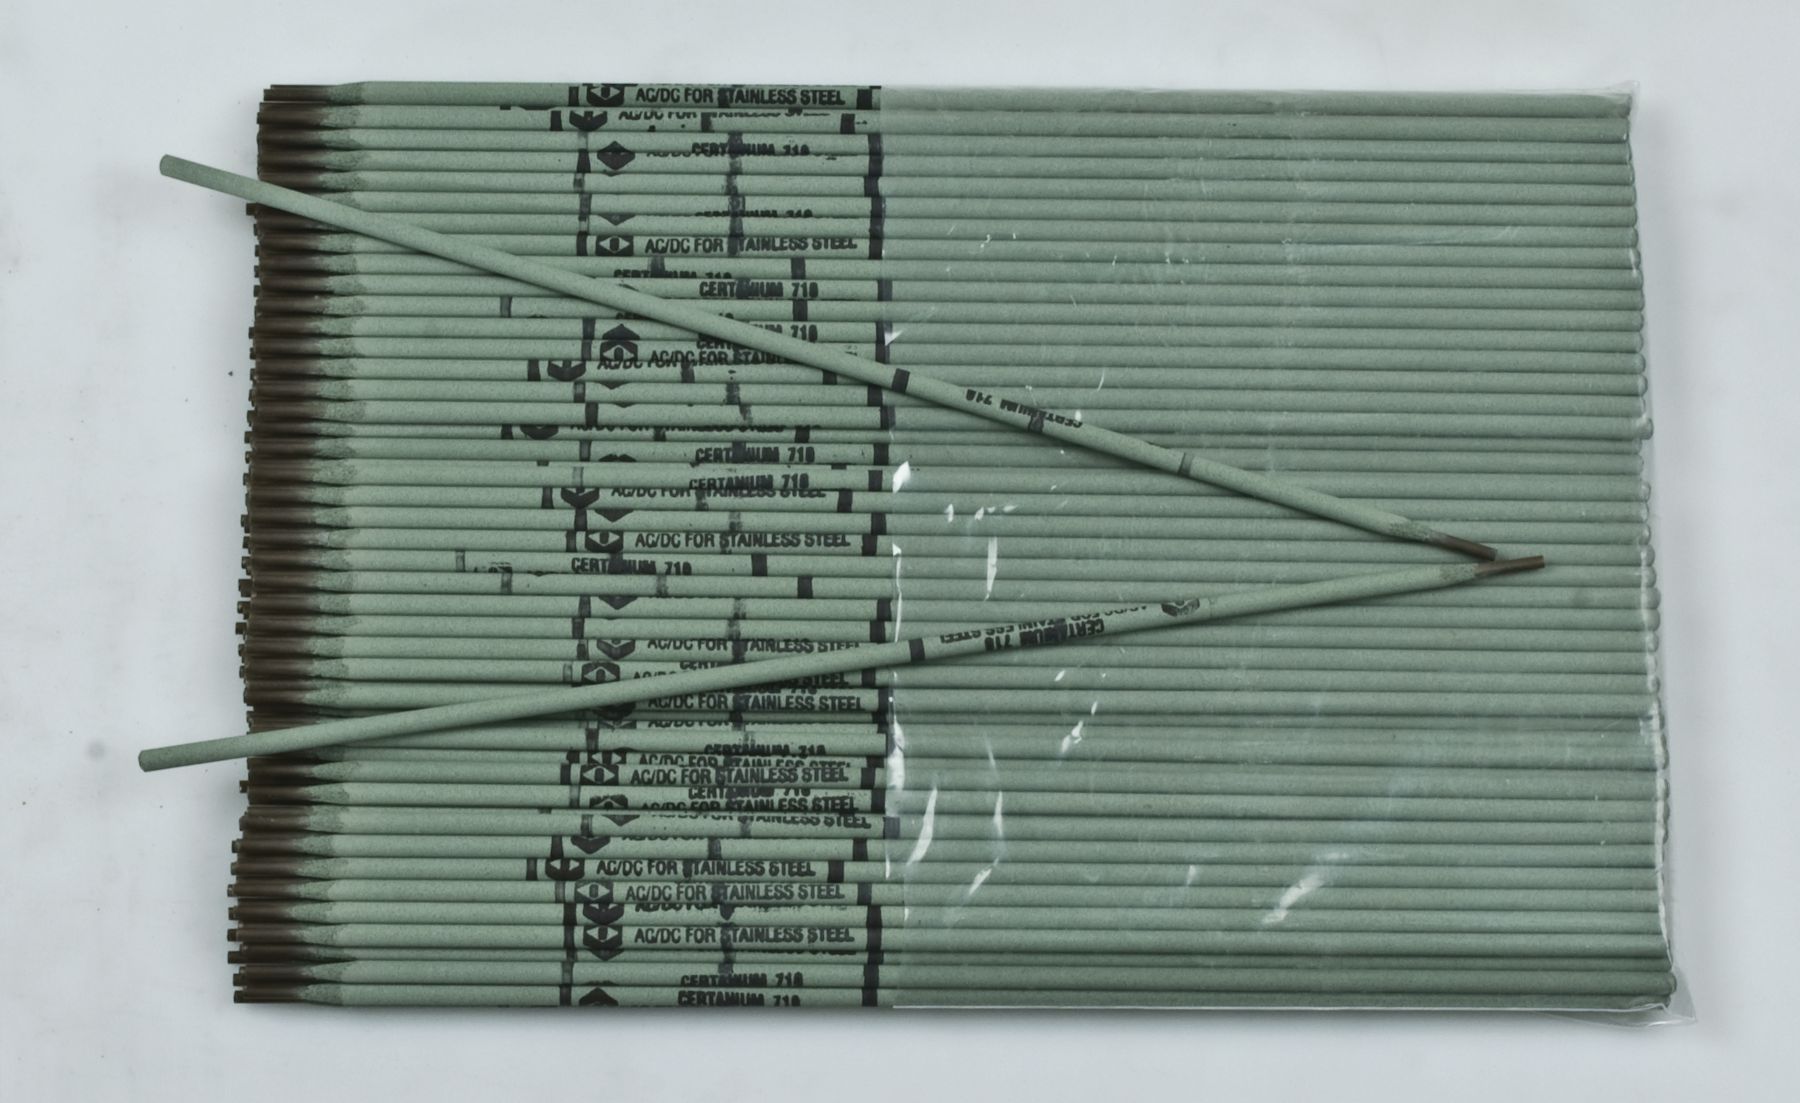
710 Stainless Steel Electrode 3/32"
$0.00
Couldn't load pickup availability
Heat Stick 650F Degrees
$0.00
Couldn't load pickup availability
Product Description
Easily joins white and pot metals.Superior Advantages
• Lead- and cadmium-free
• Extremely low melting point
• Two times stronger than ordinary solder
Low temperature, dissimilar pot metal
Tensile Strength: 17,500 PSI
Application Temperature: 360°F (182°C)
Recommended Flux: F53
Typical Applications
• Air conditioning and refrigeration units
• Brazing/soldering of copper to aluminum, brass to steel, stainless to zinc, etc.
Usage ProcedureBase metal must supply heat, as a direct flame is unworkable. A carburizing flame should be used. A flux is required for all applications where good bonding is desired.
Technical TipDo not direct torch at flux, as it will char. Allow CRONABRAZE 53 to solidify before quenching and removing flux residue. CRONASOLV™ F53 flux is recommended for all applications.
Technical Specifications
| Item#: | CW1017 |
|---|---|
| Welding Process | Brazing |
| Type | Bare Brazing Rod |
| Diameter | 1/8 " |
| Length | 18 " |
| Tensile Strength | 17,500 PSI |
| Melting Temperature | 360 °F |
| Base Metal | Pot Metal |
| Recommended Flux | F53 |
| UNSPSC #: | 23271804 |
| TAA Compliant: | Yes |
| Weight: | 2.25 lb |


